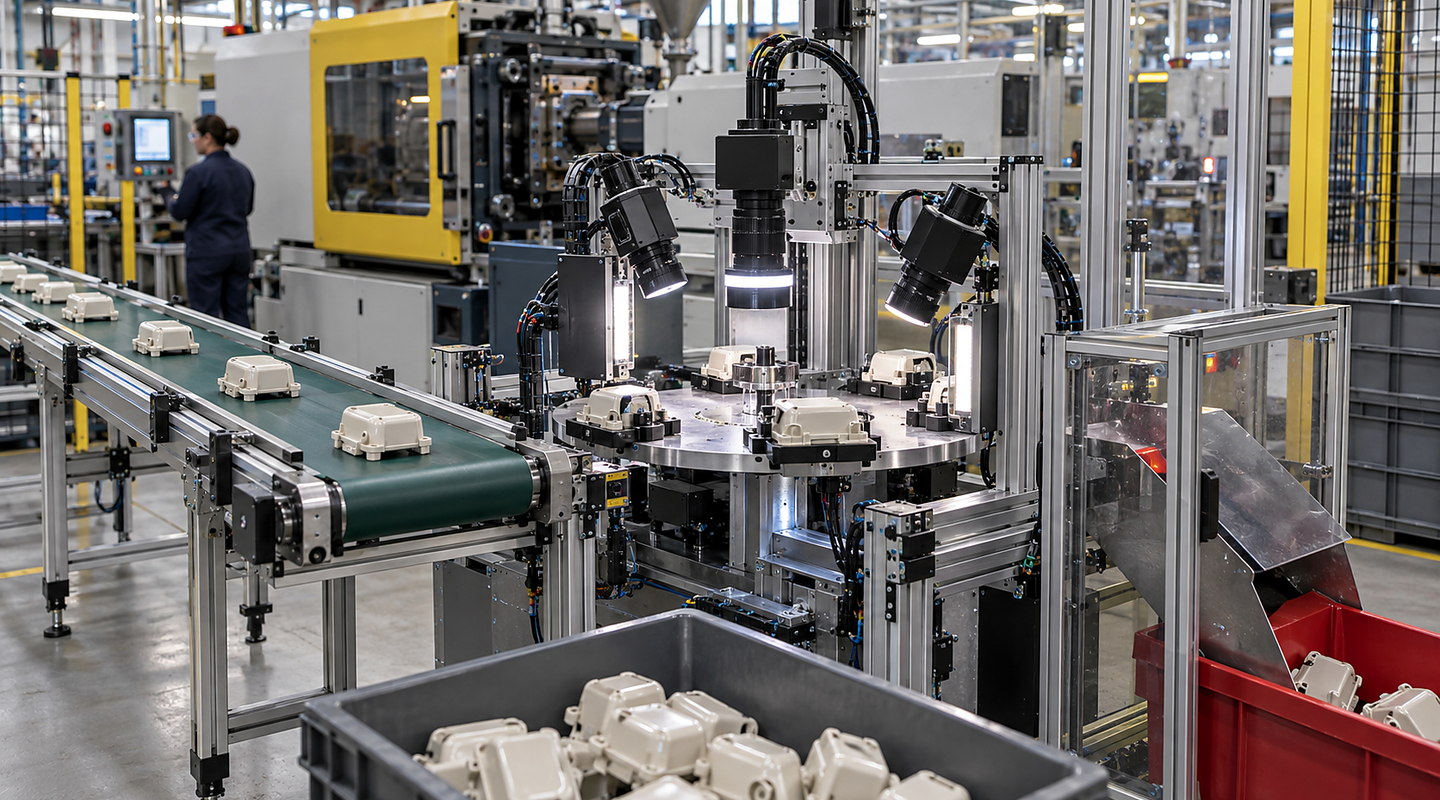
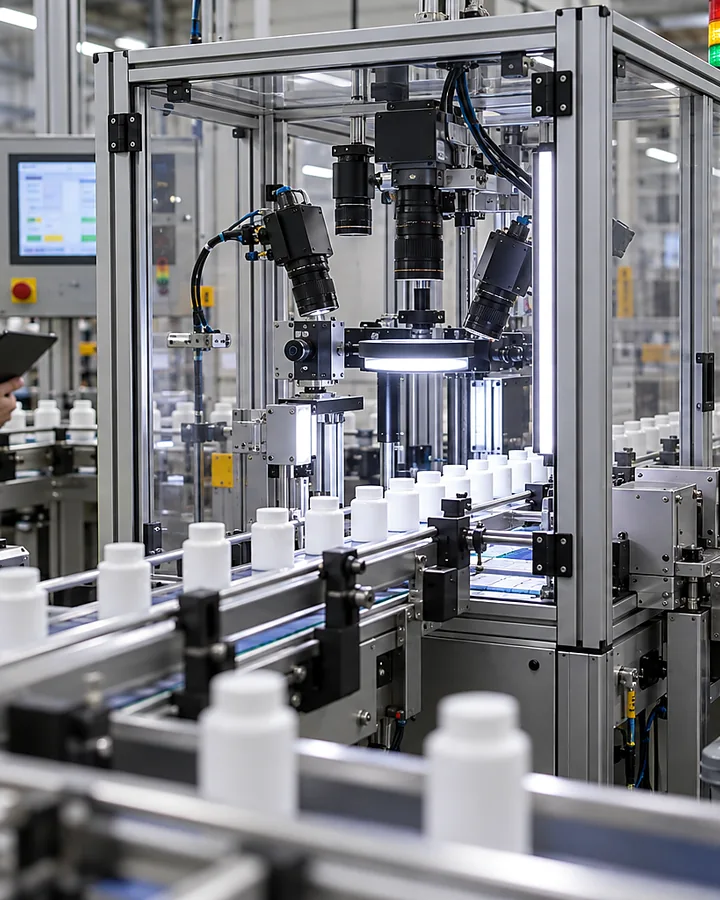
Visible Defect or Measurement Definition for Visible Surface-Defect Inspection: Defect and sample study
How should visible defect or measurement definition for visible surface-defect inspection be investigated before specifying visible surface defect inspection?
In brief
A visible mark becomes a defect when it falls outside an agreed acceptance requirement. Define the feature, its location, the permitted surface variation and the viewing conditions used to judge it. A request to detect every defect gives no usable boundary for a surface-inspection trial.
For in-line inspection using visible surface-defect inspection, describe the realistic range and how changes in visible defect or measurement definition for visible surface-defect inspection affect the result you need.
On the production floor
Turn your production information into clearer decisions — Visible Surface Defect Inspection
Plan visible surface defect inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Use this guide to resolve visible defect or measurement definition for visible surface-defect inspection before it limits the final system.
Visible Defect or Measurement Definition for Visible Surface-Defect Inspection: condition, range and effect on your process
Current condition
Record how quality staff currently distinguish an acceptable surface from a reject. Keep a physical example or agreed reference for each decision, identify the relevant area and flag disagreements before using those samples to adjust the inspection.
Realistic range
Include permitted colour, texture, coating and supplier-batch variation, together with faults near each acceptance boundary. Keep samples with an unresolved quality decision separate; the inspection cannot be judged against a reference that has not been agreed.
Effect on the system
A required area hidden by the part or fixture is outside the demonstrated view. Record that gap and investigate presentation, additional views or a separate check; do not treat an unavailable view as evidence of an acceptable surface.
Before you contact us
Five questions about visible defect or measurement definition for visible surface-defect inspection for your application
Who can confirm this information?Identify the person responsible for visible defect or measurement definition for visible surface-defect inspection in production, quality, engineering or operations.
How representative is the sample?Include age, supplier, batch, environment and upstream process state where they affect visible surface defect inspection.
What is the difficult condition?Include the slow, reflective, flexible, dirty, damaged, marginal or uncommon case that your system must still handle.
How will you judge the result?Agree the method, repetitions, acceptable range, result record and the response if the observed result falls outside the agreed range.
What else must be coordinated?Your final visible surface defect inspection scope must also account for recipe, reject and line-control interfaces, false-accept, false-reject and challenge criteria, current regulations and the conditions at your site.
Connected details
Review visible defect or measurement definition for visible surface-defect inspection as part of the complete system
Question 1
Visible Defect or Measurement Definition for Visible Surface-Defect Inspection
If the requirement is a measurement, state the feature, units, reference method and acceptance limits separately from a presence or appearance decision. The trial must establish whether that measurement is supported on the actual surface; a visible mark alone does not establish its depth or a hidden property.
Question 2
Good, Bad and Marginal Sample Range
For Visible Defect or Measurement Definition for Visible Surface-Defect Inspection: Defect and sample study, describe the current position, required outcome, acceptable limits and known exceptions for good, bad and marginal sample range. That lets us compare options against your real production rather than one nominal value.
Question 3
Part Presentation and Production Speed
For Visible Defect or Measurement Definition for Visible Surface-Defect Inspection: Defect and sample study, describe the current position, required outcome, acceptable limits and known exceptions for part presentation and production speed. That lets us compare options against your real production rather than one nominal value.
Question 4
Optics, Lighting and Environmental Conditions
For Visible Defect or Measurement Definition for Visible Surface-Defect Inspection: Defect and sample study, describe the current position, required outcome, acceptable limits and known exceptions for optics, lighting and environmental conditions. That lets us compare options against your real production rather than one nominal value.
Question 5
Recipe, Reject and Line-Control Interfaces
For Visible Defect or Measurement Definition for Visible Surface-Defect Inspection: Defect and sample study, describe the current position, required outcome, acceptable limits and known exceptions for recipe, reject and line-control interfaces. That lets us compare options against your real production rather than one nominal value.
Question 6
False-Accept, False-Reject and Challenge Criteria
For each defect class, retain the agreed reference decision, inspected area and relevant finish variants. Record missed defects and false rejects separately from unresolved results. Use the acceptance guide to turn those definitions into a challenge record.