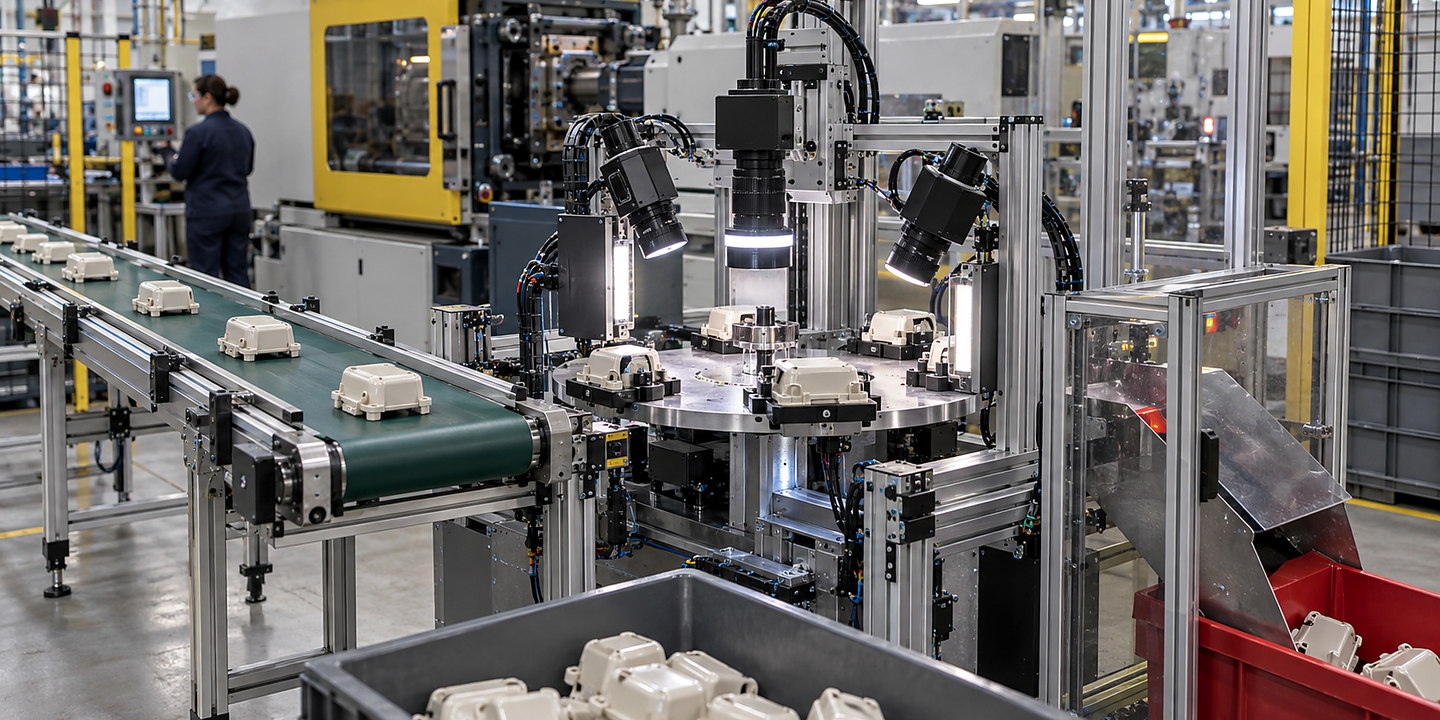
Plan mechanical, electrical, control, data, safety and operator interfaces for visible surface defect inspection.
In brief
An inspection interface must keep the part, selected recipe, image result and agreed reject or review action connected. Define who handles missing or late results, uncertain classifications and recovery. A camera decision alone does not prove that the correct part was controlled.
For retrofit or multi-variant checks involving visible surface-defect inspection, define every physical connection, signal, responsibility, check and fallback before installation.
On the production floor
Connect equipment, controls and people into one reliable process — Visible Surface Defect Inspection
Plan visible surface defect inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Your integration review should connect part presentation and production speed, optics, lighting and environmental conditions and the people who run the process.
Six areas to coordinate for visible surface defect inspection
Mechanical
Confirm the part position and mounting arrangement for each required view, including areas hidden by guides or fixtures. Allow for the agreed lighting, reject location and access for cleaning or maintenance without assuming that a view will remain unchanged after adjustment.
Electrical
For Visible Surface Defect Inspection, list the supplies, isolation, protective devices, panels and cable routes required by the proposed installation.
Controls
Agree the sequence for part arrival, recipe confirmation, image capture, result availability and the required part action. State the permitted timing and the response to a missing image, unavailable result or interrupted cycle; these are requirements to verify with the line controls.
Safety
Review risk controls, stop behaviour, access, reset and the checks needed around optics, lighting and environmental conditions.
Data
Specify which part or batch identifier, recipe revision, image or result record must be retained, for how long and by whom. Distinguish a valid acceptance decision from an unresolved or unavailable result. Do not assume an interface or data-retention capability until its scope is agreed.
Your team
Plan normal operation, replenishment, clearance, cleaning, maintenance and training for retrofit or multi-variant checks involving visible surface-defect inspection.
How the work comes together
Plan fault recovery for in-line inspection using visible surface-defect inspection as carefully as normal running
For Visible Surface Defect Inspection, your team can review each stage before the complete installation is put into routine use.
01
Define the Visible Decision and Collect Representative Samples
Share representative good, bad and marginal samples, including the normal range for visible defect or measurement definition for visible surface-defect inspection and the difficult good, bad and marginal sample range cases.
02
Prove Contrast, Presentation and Timing in an Optical Trial
Compare suitable methods and use focused trials to show how each option performs against part presentation and production speed.
03
Integrate Cameras, Controls, Reject Handling and Recipes
Connect the equipment to your line, services and controls while resolving optics, lighting and environmental conditions for day-to-day operation.
04
Challenge Marginal Cases and Document Agreed Results
Confirm recipe, reject and line-control interfaces, then complete and record false-accept, false-reject and challenge criteria before your operating team takes over.
For your application: agree how affected parts remain identifiable after an interrupted inspection or reject sequence, who authorises recovery and which checks precede resumed production. Include those actions in the acceptance plan.
Important limits
Line connections can change the approach for Visible Surface Defect Inspection
A camera can only assess a property made visible and repeatable by the inspection setup.
Sample diversity and marginal cases determine how meaningful a feasibility result is.
Visual inspection does not replace hidden, destructive, functional or statutory tests.